How Do Laminated Trays Achieve Reliable Heat Sealing with Lid Film?
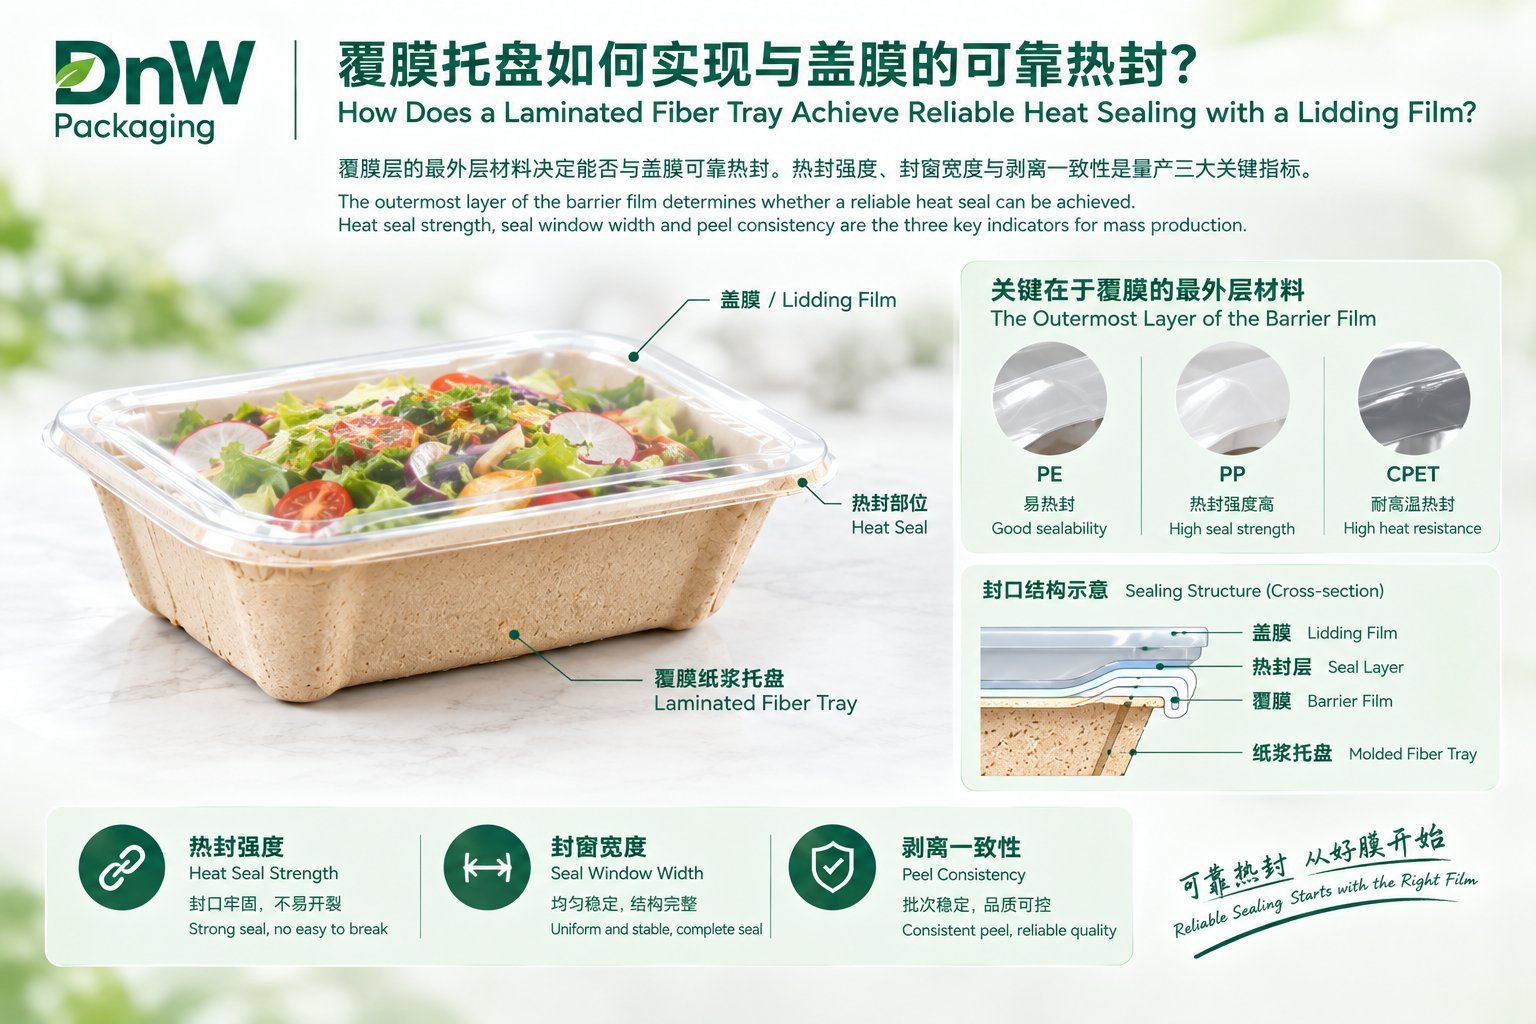
The outermost laminate material determines whether the tray seals reliably to a lid film. Seal strength, seal-window width and peel consistency are the three key production metrics.
Heat-Seal Essentials
Sealant layer choice
A PE/PP outer layer seals directly to matching lid films.
Seal strength
Typically ≥ 15–25 N/15mm, set by product weight.
Seal window
The wider the temperature/time/pressure window, the stabler the line.
Easy-peel vs strong seal
Use peelable lid films or mechanical tear features when easy-open is required.
Typical Heat-Seal Parameters
Values per full seal cross-section.
| Seal strength target | ≥ 15–25 N/15mm (by category) |
|---|---|
| Temp window | ±15 °C or wider preferred |
| Test standard | ASTM F88 |
| Leak testing | ASTM F1929 / water bath |
| Matching lid films | PE, PP, PET/PE laminate lids |
| Production validation | Seal-window curve + sampled leak checks |
Heat-Seal FAQ
Fiber tray surfaces are uneven — will they seal?
The laminate fills surface porosity; seal quality depends on film integrity and sealing parameters.
How to avoid seal leaks?
Map the seal window, keep the rim laminate intact, and run sampled leak checks.
Will our existing sealer work?
Most PE/PP systems run on standard sealers; special structures need a temperature-limit review.
Need an Assessment for Your Application?
Share your tray geometry, application and performance requirements — a DNW engineer will help evaluate film structure and process parameters.
Discuss Your Project